HEXNOVAS CASE
Welded Block Exchanger External Leakage: Repair or Replace?
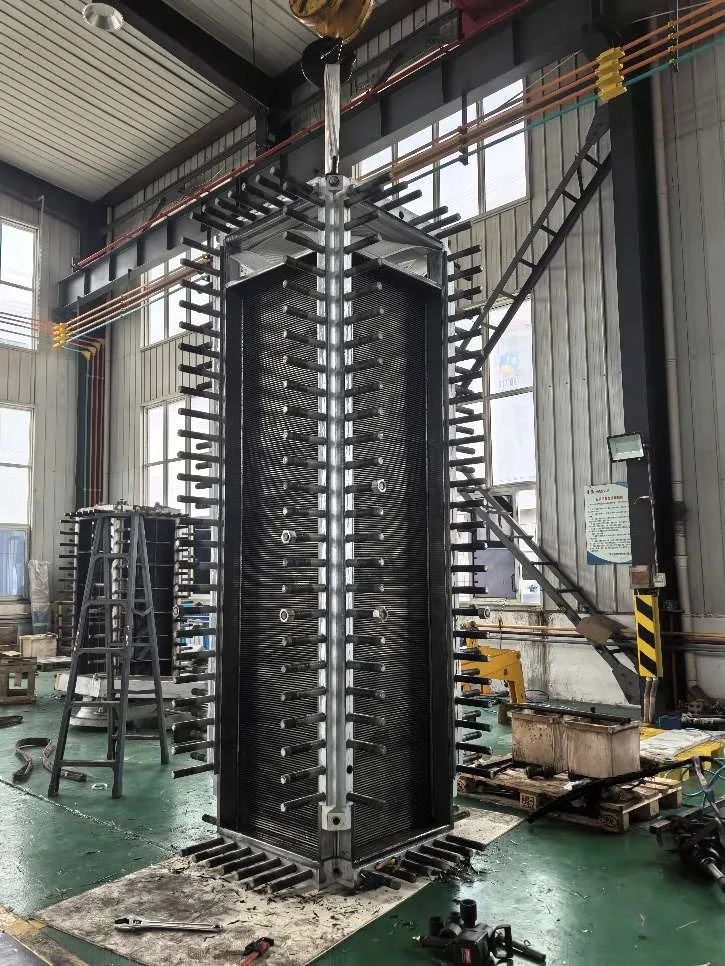
CPX75-V-500 service case: separating gasket and sealing-corner damage from internal leakage, retaining the core and verifying repair by hydraulic testing.
Project snapshot
Documented inspection and workshop test results
- Duty: petrochemical C8 aromatics heat recovery
- Equipment: vertical CPX75-V-500
- Recorded plate material: 316L
- Service decision: retain the welded core; restore the sealing interfaces
- Verification: hot- and cold-side hydraulic tests
The Decision Behind the Repair
A leak outside a welded block exchanger does not, by itself, identify a failed heat-transfer core. For this CPX75-V-500, the maintenance question was whether the fluid was escaping through the panel sealing system or through damage within the welded assembly. Those possibilities required different service scopes.
The unit was returned for a planned shutdown inspection in July 2026. The service record describes C8 aromatics heat recovery, with C8 aromatics on the hot side and C8 aromatics with toluene on the cold side. It records a hot-side temperature program of 189°C to 172.2°C and a cold-side program of 171°C to 183°C. These are recorded operating conditions, not newly measured post-repair performance.
Three Findings That Defined the Service Scope
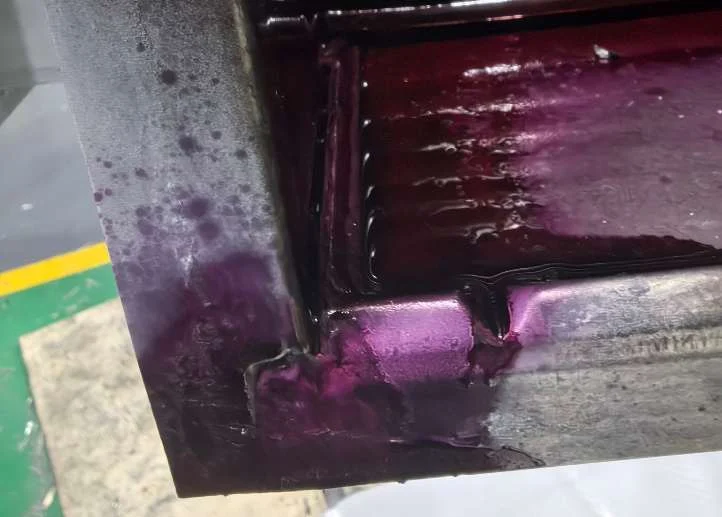
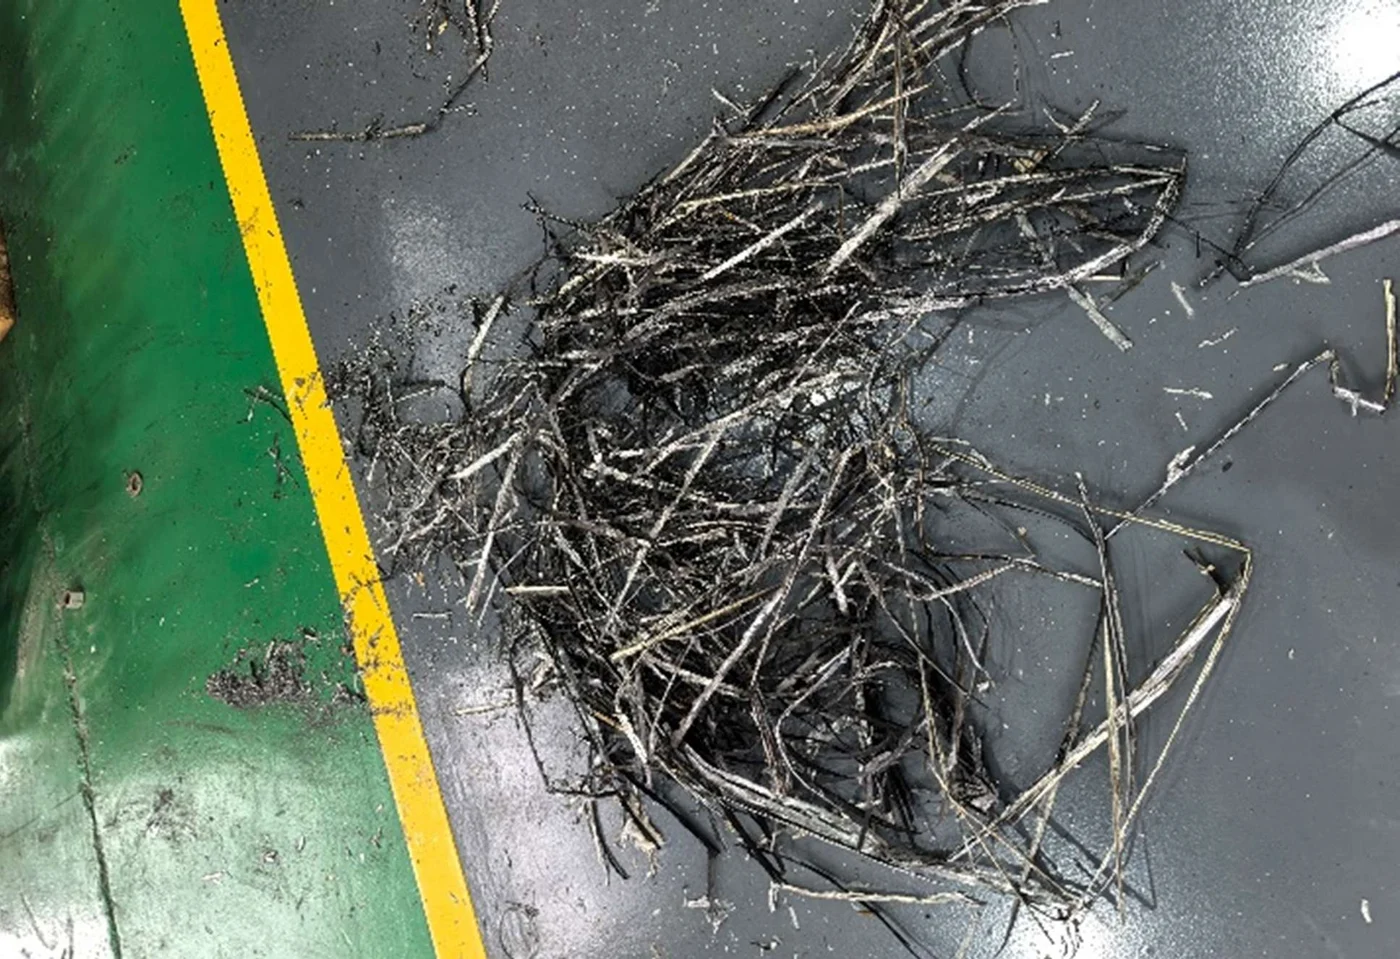
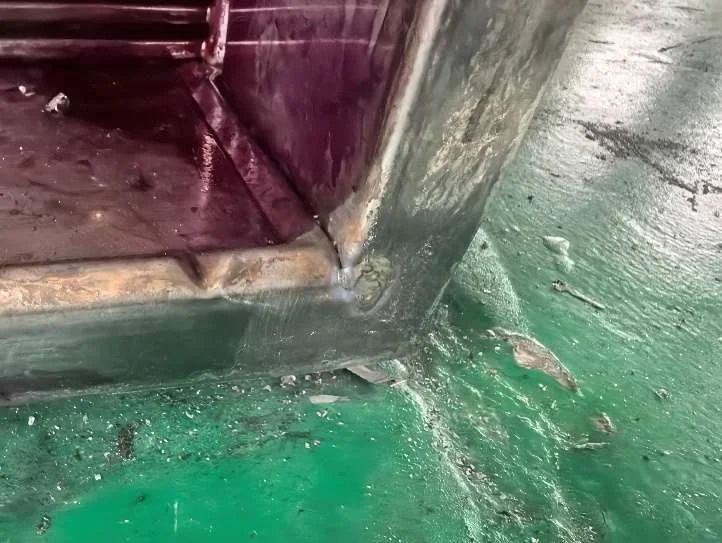
Fluid traces on the support and fragments at the panel joints directed attention to the external sealing path. Dismantling then exposed fragmented gaskets around the perimeter and deformation at all 16 sealing corners. Replacing a gasket alone would have left the damaged seating surfaces unaddressed.
The core investigation gave a different result: dye-penetrant examination did not reveal cracks explaining the leakage, and the bubble test reported no internal leakage. Together, these findings supported a localized repair of the sealing interfaces while retaining the existing welded core.
| Inspection evidence | Relevance to the repair decision |
|---|---|
| Fragmented panel gaskets | Renew the complete panel-gasket set. |
| Deformation at 16 sealing corners | Repair and finish the corner surfaces before reassembly. |
| No internal leakage reported in the bubble test | The recorded findings did not require an internal-leak repair. |
| No leakage-causing core cracks found by penetrant inspection | Core replacement was not selected for this documented service. |
Restoring the Joint, Not Simply Increasing Bolt Load
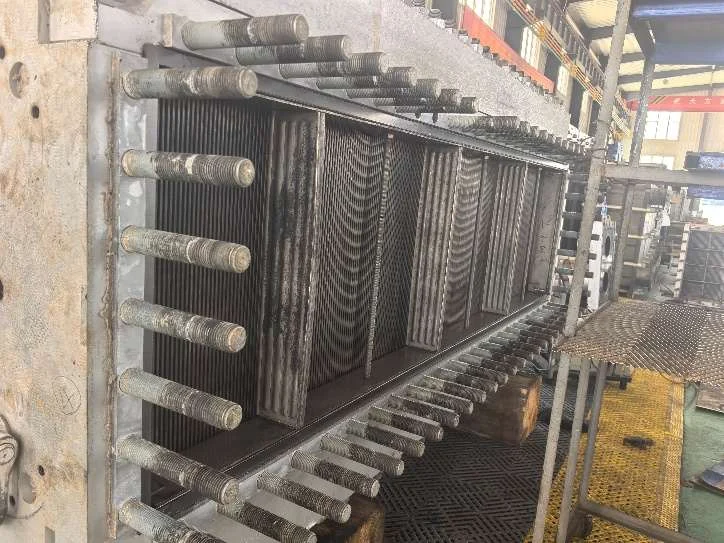
The repair covered eight sealing corners on each side. The team used argon-arc weld repair followed by grinding to restore the corner surfaces, inspected the panel linings, refitted the frame and baffle assemblies, cleaned the sealing faces and installed new panel gaskets.
Panel bolts were tightened with hydraulic tooling in three controlled passes. The subsequent gasket-compression check recorded intact gaskets without crushing. The sequence linked surface restoration, gasket renewal and controlled assembly as parts of one repair.
The report associates the damage with excessive tightening during an earlier intervention. That is the service team’s assessment; the report does not provide an independently measured history of the earlier bolt loads. It is a reason to investigate a leaking joint before tightening it further, not proof that every similar leak has the same cause.
What the Hydraulic Tests Established
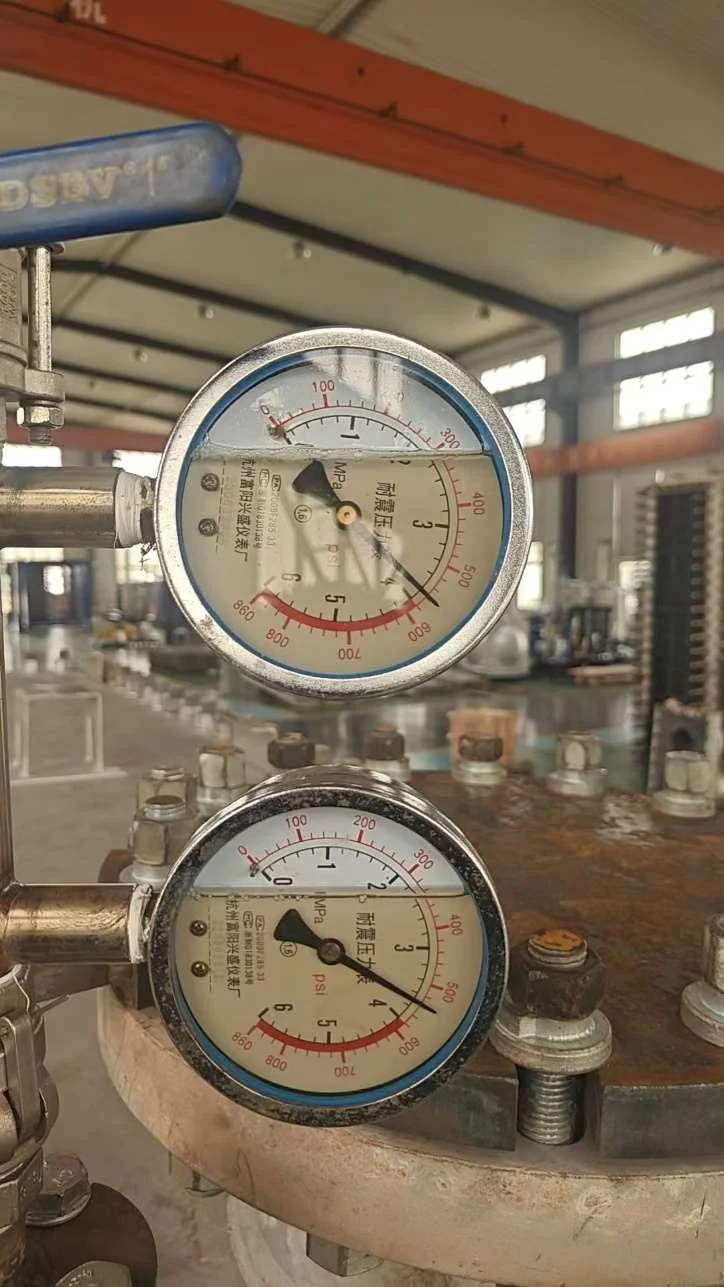
The separate hydraulic test sheet records a gradual pressure increase using demineralized water with chloride content below 10 ppm. Each side was held for 30 minutes, with an accepted result entered for both tests.
| Recorded test | الضغط | Hold | Result |
|---|---|---|---|
| Hot side / A1 | 38.0 bar | 30 minutes | Accepted |
| Cold side / B2 | 31.0 bar | 30 minutes | Accepted |
Where the Evidence Ends
The documented outcome is a repaired and reassembled exchanger that passed the recorded workshop hydraulic tests and was prepared for dispatch. The report does not include operating measurements after restart, a restored heat-duty measurement or a quantified reduction in downtime or cost.
Test pressure is not a continuous operating rating. The general-data pressure entries contain inconsistent unit notation, so they are not reproduced here as an approved design-pressure specification. The nameplate and approved equipment documents must be checked for any subsequent service decision.
The recorded torque and start-up recommendations apply to this equipment and service context. They are not provided as a universal procedure for other exchangers. A comparable unit needs its own approved assembly and operating instructions.
Prepare the Next Maintenance Decision
For an externally leaking block exchanger, a useful enquiry separates the observed symptom from the requested spare part. Identify exactly where leakage appears, whether cross-contamination has been detected, when it began and what tightening or maintenance has already been attempted.
HEXNOVAS can review that information alongside the equipment identification and process conditions to define the next engineering review. This case supports inspection-led repair planning; it does not establish that every leaking core can be retained or that parts are interchangeable across a model family.
Source record: WHE Service Report 26416-E602 and Hydraulic Test Report HTR-26416-E-602, issued by Yangzhou Panstar Heat-Exchanger Equipment Co., Ltd. Photographs and recorded findings are taken from that service record. This HEXNOVAS case analysis focuses on maintenance decisions and the limits of the test evidence.