Plate preparation
Sheet grade, thickness and geometry are selected for the process and mechanical design.
One plate, infinite possibilities
HEXNOVAS manufactures custom laser-welded pillow plates for tank jackets, immersion cooling and falling-film chillers. Compare single- and double-embossed construction and request project sizing.
Request Pillow Plate Design Review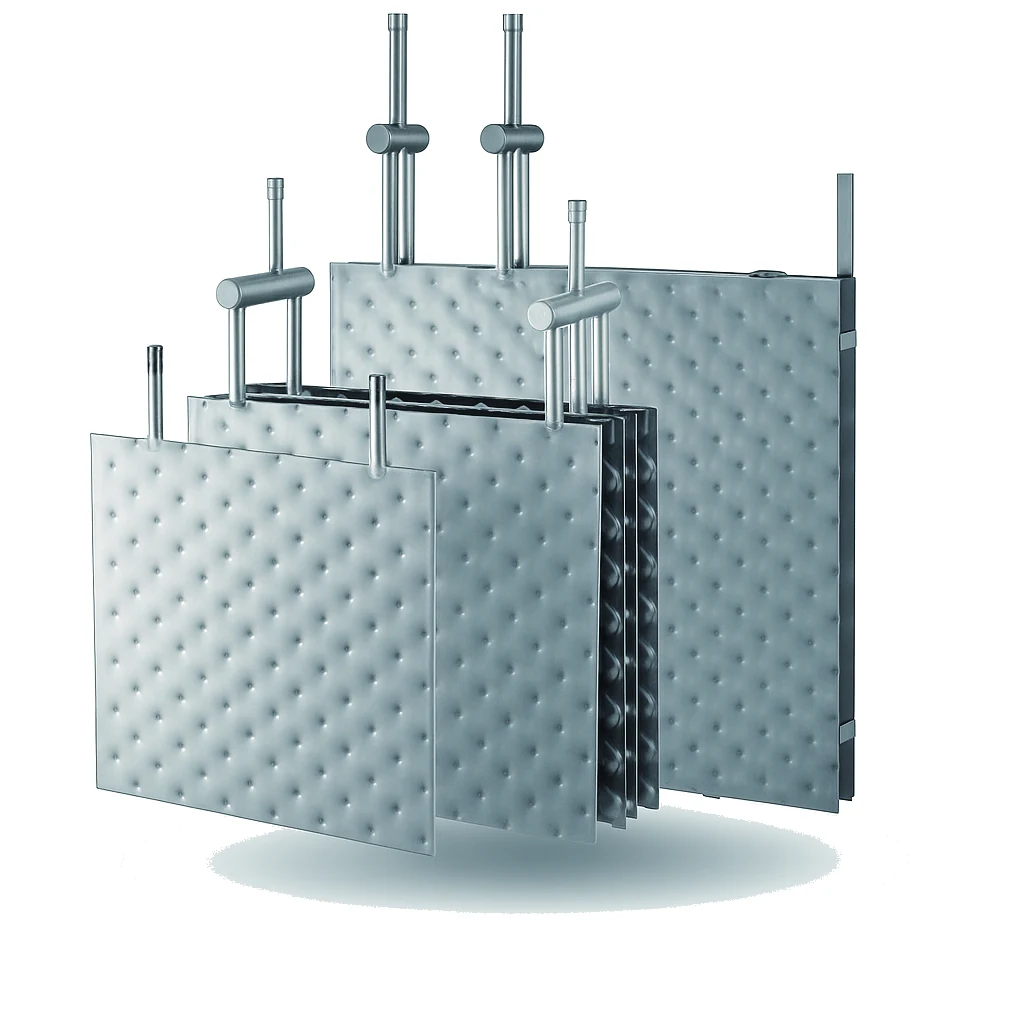
How pillow plates are made
Two metal sheets are laser-welded in a calculated pattern. The welded plate pair is then inflated under controlled high pressure, creating pillow-shaped channels that distribute the heating or cooling medium across a broad surface.
The finished surface can operate as a vessel jacket, an immersed plate bank, a falling-film surface or a custom thermal component.
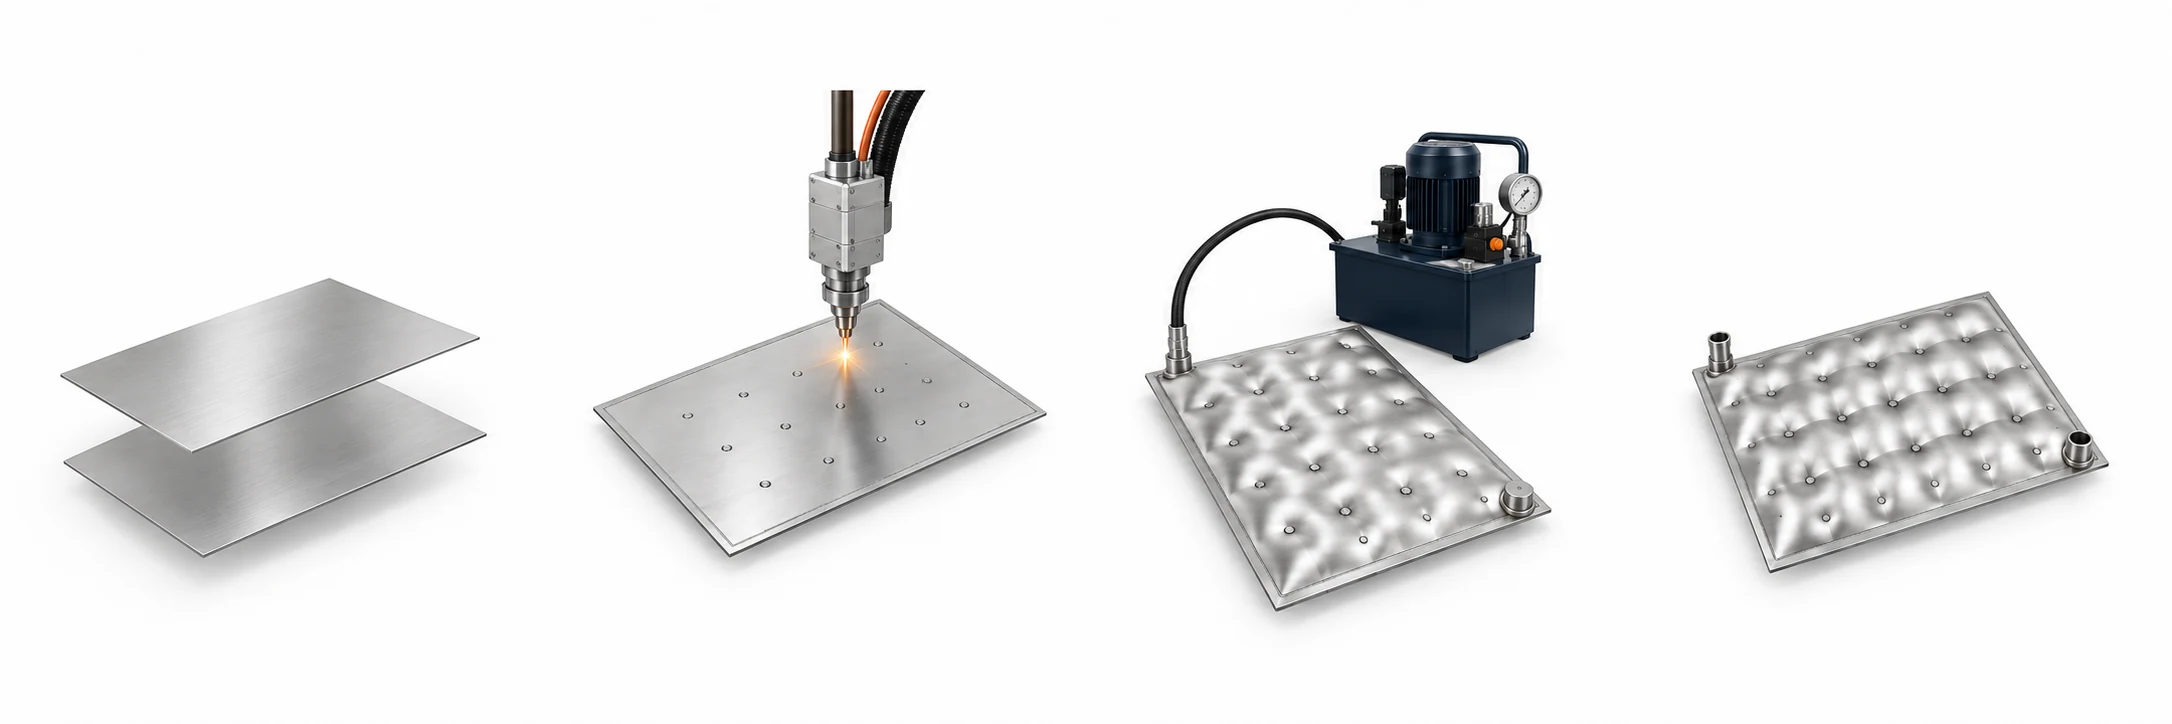
Sheet grade, thickness and geometry are selected for the process and mechanical design.
A project-specific spot and perimeter weld pattern defines the future flow channels.
Controlled pressure forms the channels and establishes the required pillow depth.
Connections, forming, fabrication and inspection complete the application-ready surface.
Working principle · 3D animation
360° interactive view: Drag the model to inspect it from every angle.
Explore laser welding, perimeter sealing and hydraulic inflation. Compare single- and double-embossed plates, pause any stage and rotate the model.
Conceptual 3D illustration. Weld patterns, sheet thicknesses and forming parameters are confirmed for each project.
Working principle · 3D animation
360° interactive view: Drag the model to inspect it from every angle.
Open the cabinet, inspect the distribution pan and follow separate water and cooling circuits through a falling film plate chiller.
Conceptual 3D illustration. Distribution, refrigerant feed and collection arrangements are application-specific.
Working principle · 3D animation
360° interactive view: Drag the model to inspect it from every angle.
Inspect the smooth product wall, single-sided pillow inflation and independent jacket circuit. Follow heat transfer through the vessel wall.
Conceptual 3D illustration. Integrated welded jacket shown. Cutaway views explain construction; welded layers do not separate in service.
Working principle · 3D animation
360° interactive view: Drag the model to inspect it from every angle.
Explore wide gas passages, the independent recovery-liquid circuit and offline wash-down of the pillow plate bank.
Conceptual 3D illustration. Wide spacing reduces blockage risk; it does not eliminate fouling. Washing is shown with gas isolated and equipment cooled.
Why pillow plates
Inflated channels promote turbulence and improve thermal performance.
Smooth stainless-steel process surfaces support hygienic design and effective cleaning.
Large heat-transfer areas can be built into tanks, walls and restricted spaces.
Panel shape, dimensions, dimple depth, connections and weld pattern are project-specific.
The active plate body is fully welded and contains no gaskets.
Laser-welded plate pairs can be engineered for demanding pressure and temperature conditions.
Plate construction
The plate construction is selected according to the required process surface, installation method and pressure design.
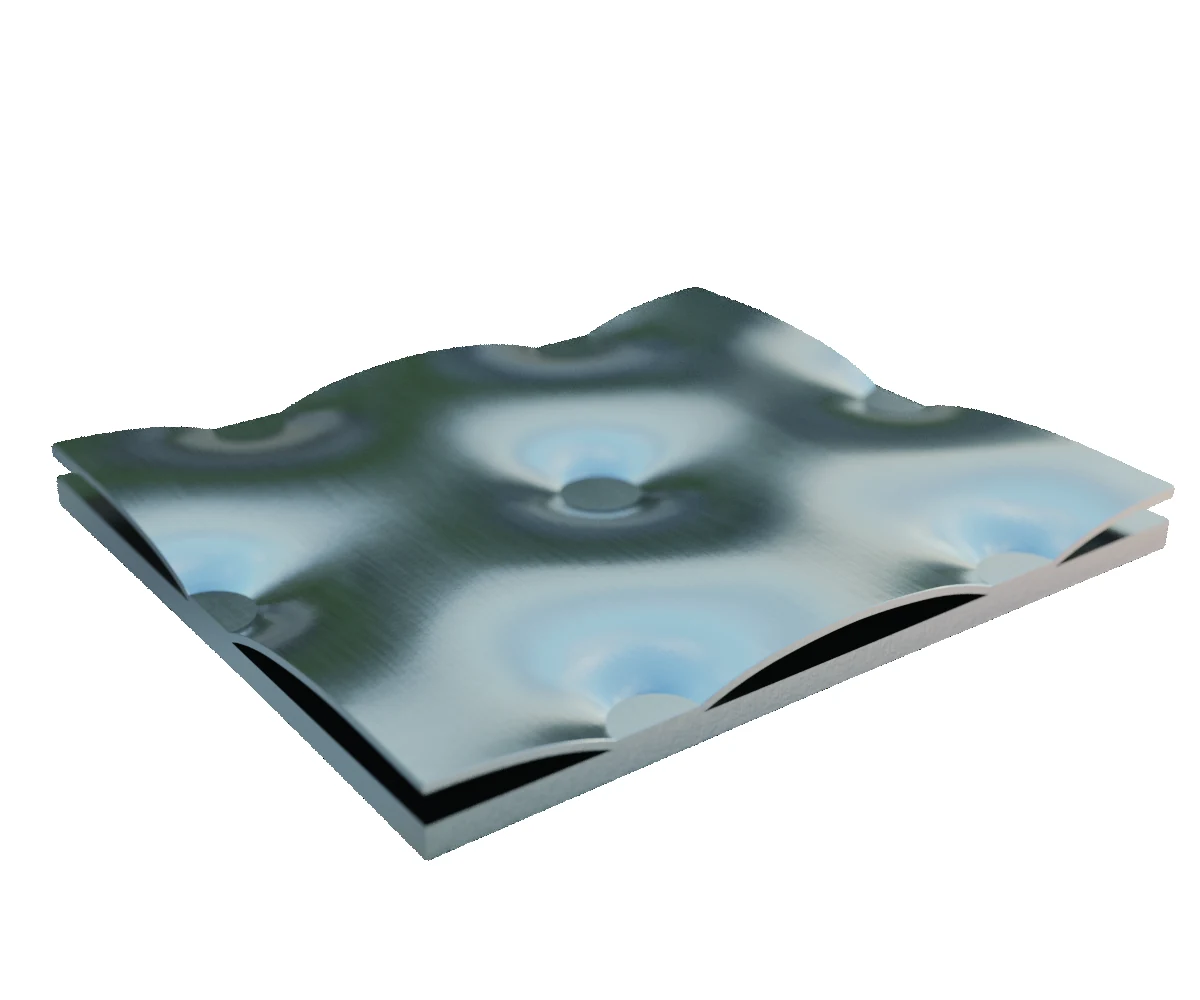
Two sheets with different thicknesses are welded and inflated so the thicker process side remains flat. This makes the construction well suited to vessel shells, tank bottoms and hygienic product-contact surfaces.
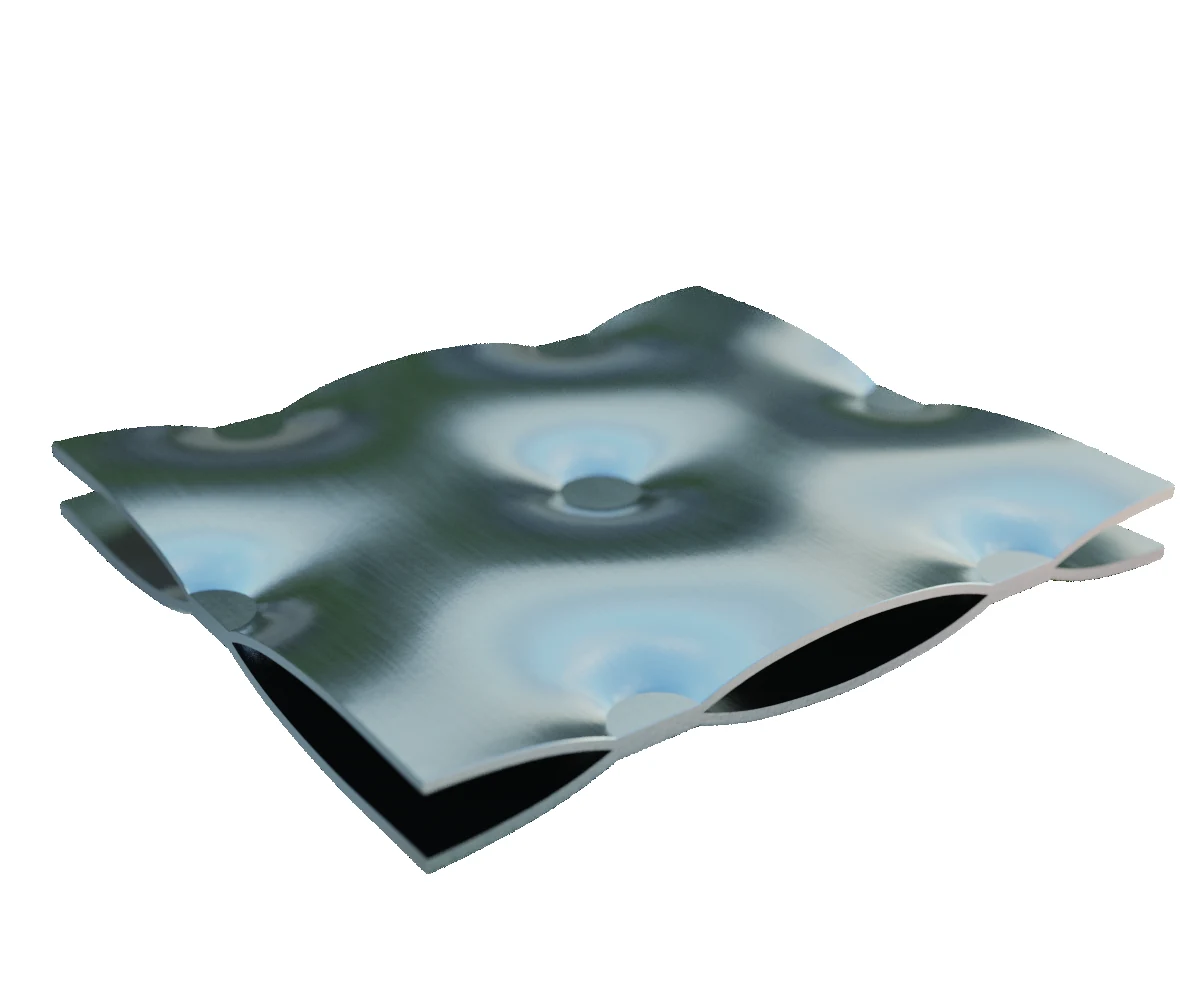
Two sheets of similar thickness expand on both sides during inflation. The resulting symmetrical channel is ideal when a flat external surface is not required.
Engineering range
Final plate thickness, inflation depth, weld pattern and allowable pressure are confirmed by project-specific thermal and mechanical calculations.
Allowable pressure must be confirmed for each project against operating temperature, material, sheet thickness, weld pattern and applicable code requirements.
Certification and documentation scope, including CE/PED where applicable, is agreed for each order.| Flat side | Inflated side |
|---|---|
| 2.0 mm | 0.8 mm |
| 2.5 mm | 0.8 mm |
| 3.0 mm | 0.8 / 1.0 mm |
| 4.0-6.0 mm | 0.8 / 1.0 / 1.25 / 1.5 mm |
| 8.0-30 mm | 1.25 / 1.5 / 2.0 / 2.5 mm |
| First side | Second side |
|---|---|
| 0.8 mm | 0.8 mm |
| 1.0 mm | 1.0 mm |
| 1.25 mm | 1.25 mm |
| 1.5 mm | 1.5 mm |
| 2.0-2.5 mm | 2.0-2.5 mm |
Forms and structures
Pillow plates can be rolled, formed, segmented and assembled to follow the equipment geometry.
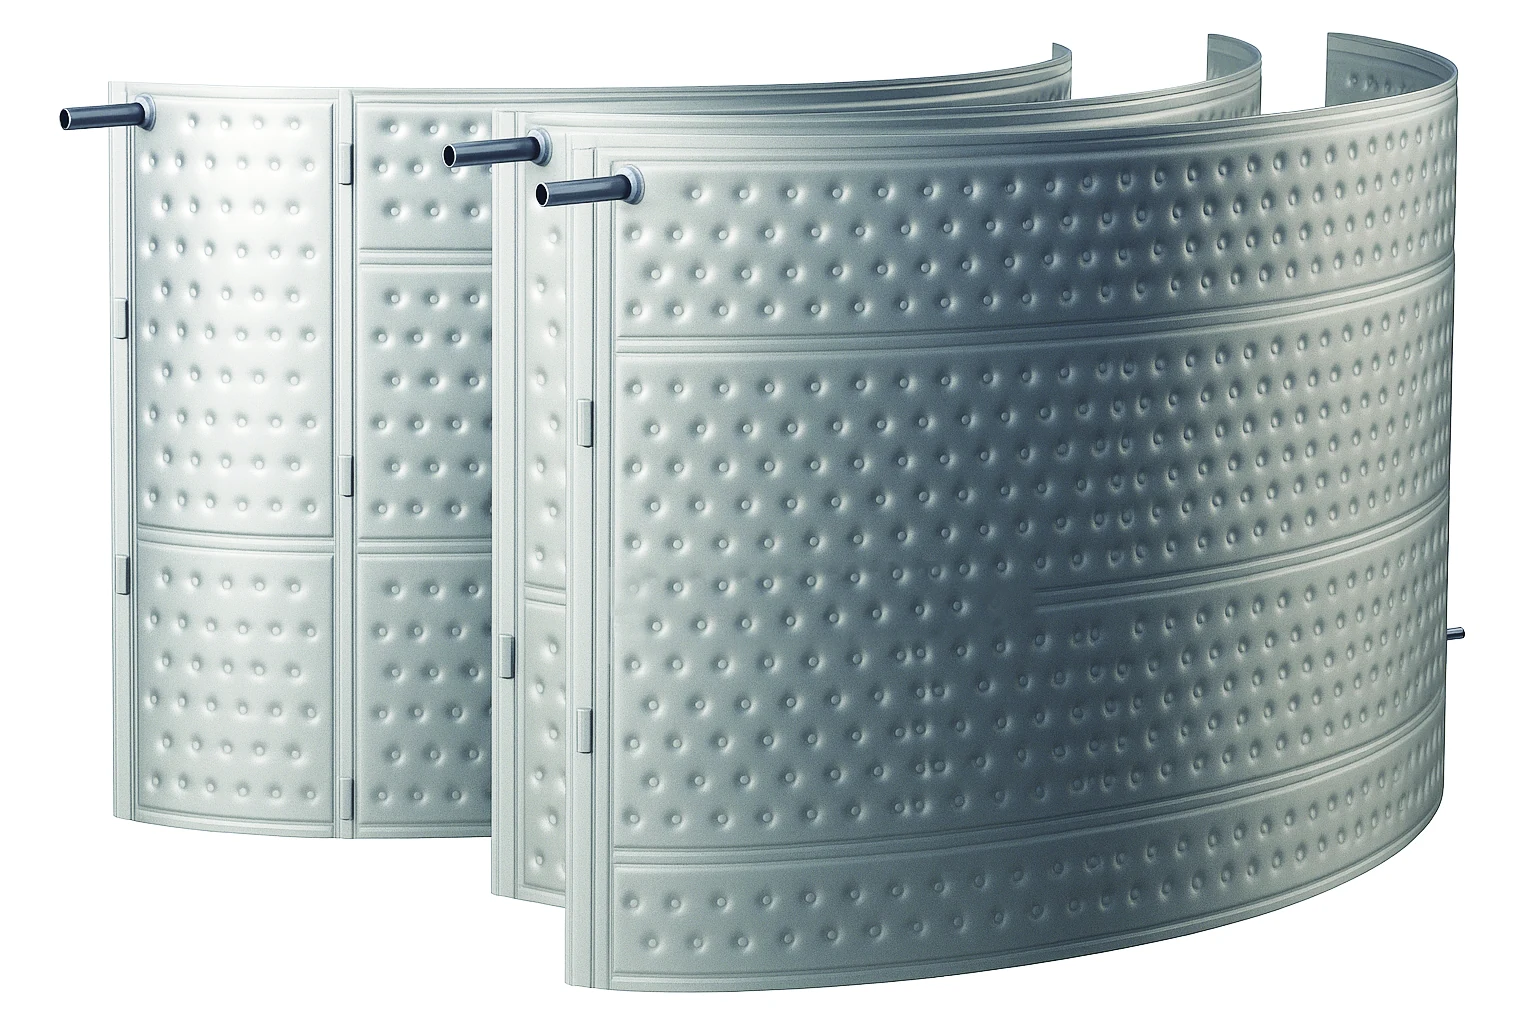
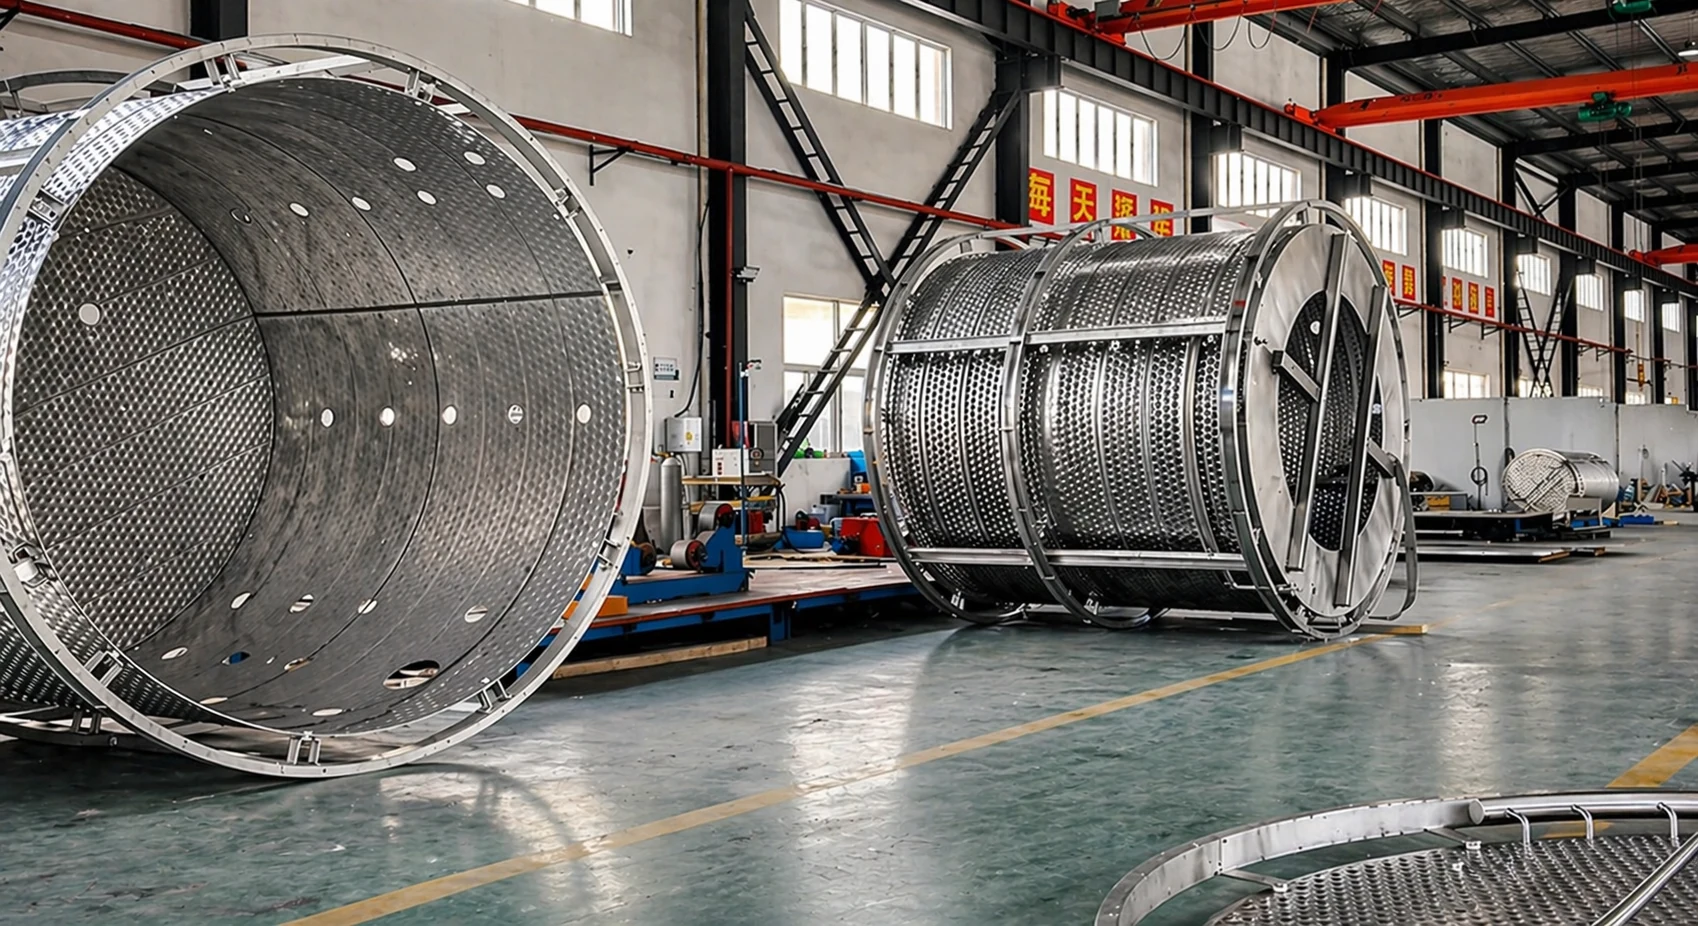
Formed pillow panels follow cylindrical vessel walls for direct heating or cooling.
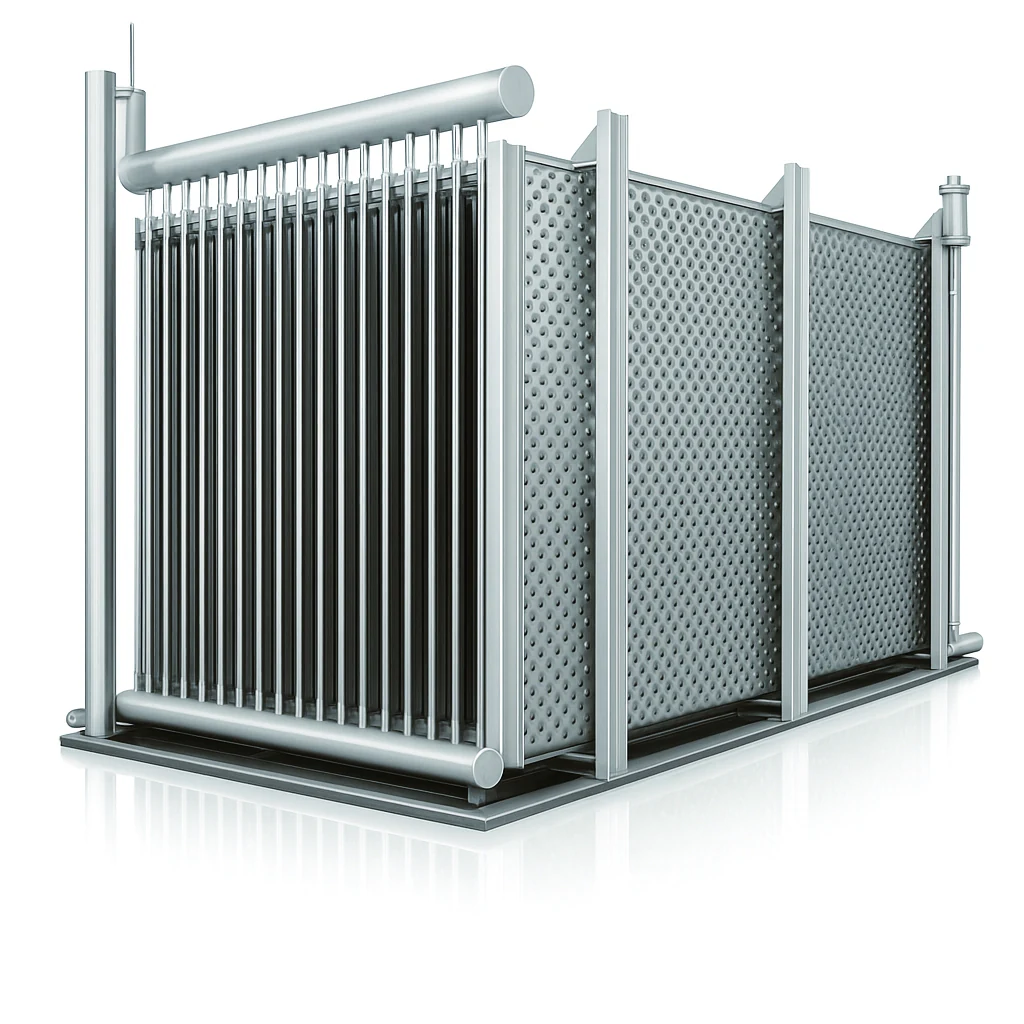
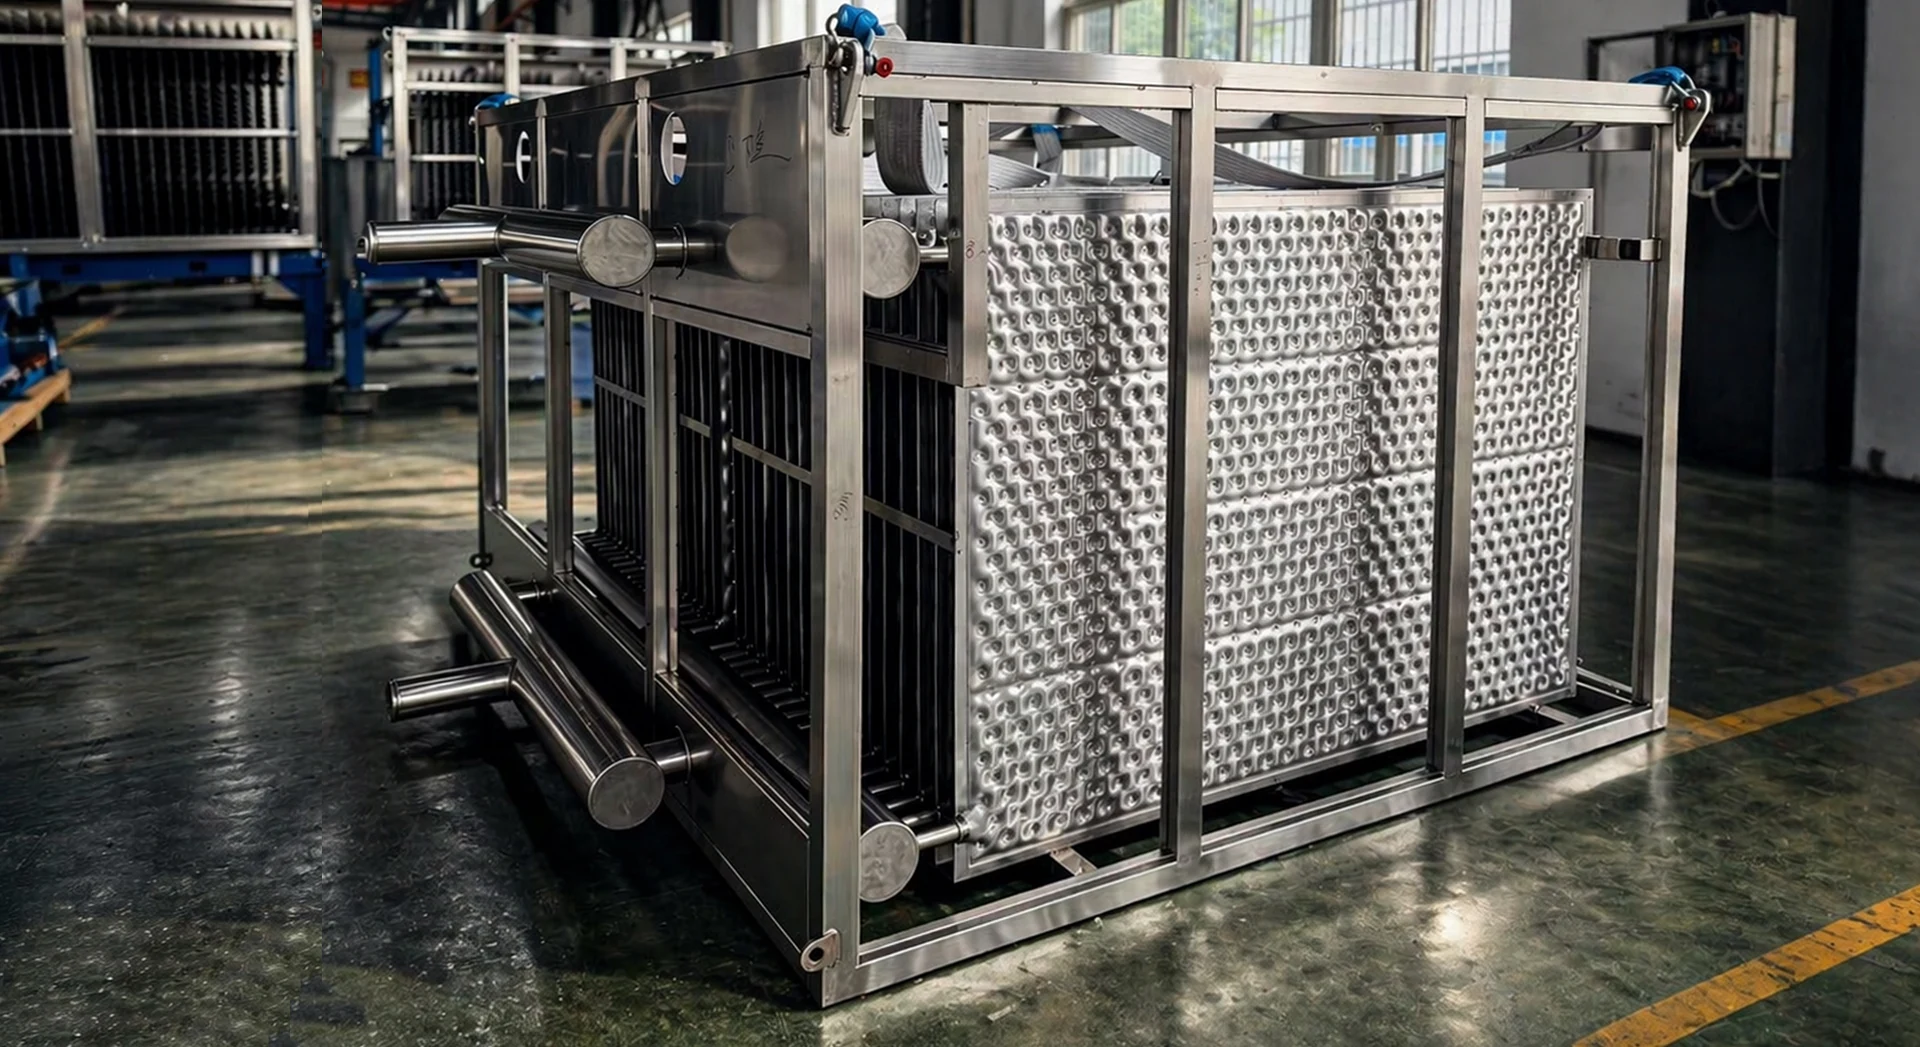
Parallel pillow plates provide high surface area for immersion and heat-recovery duties.
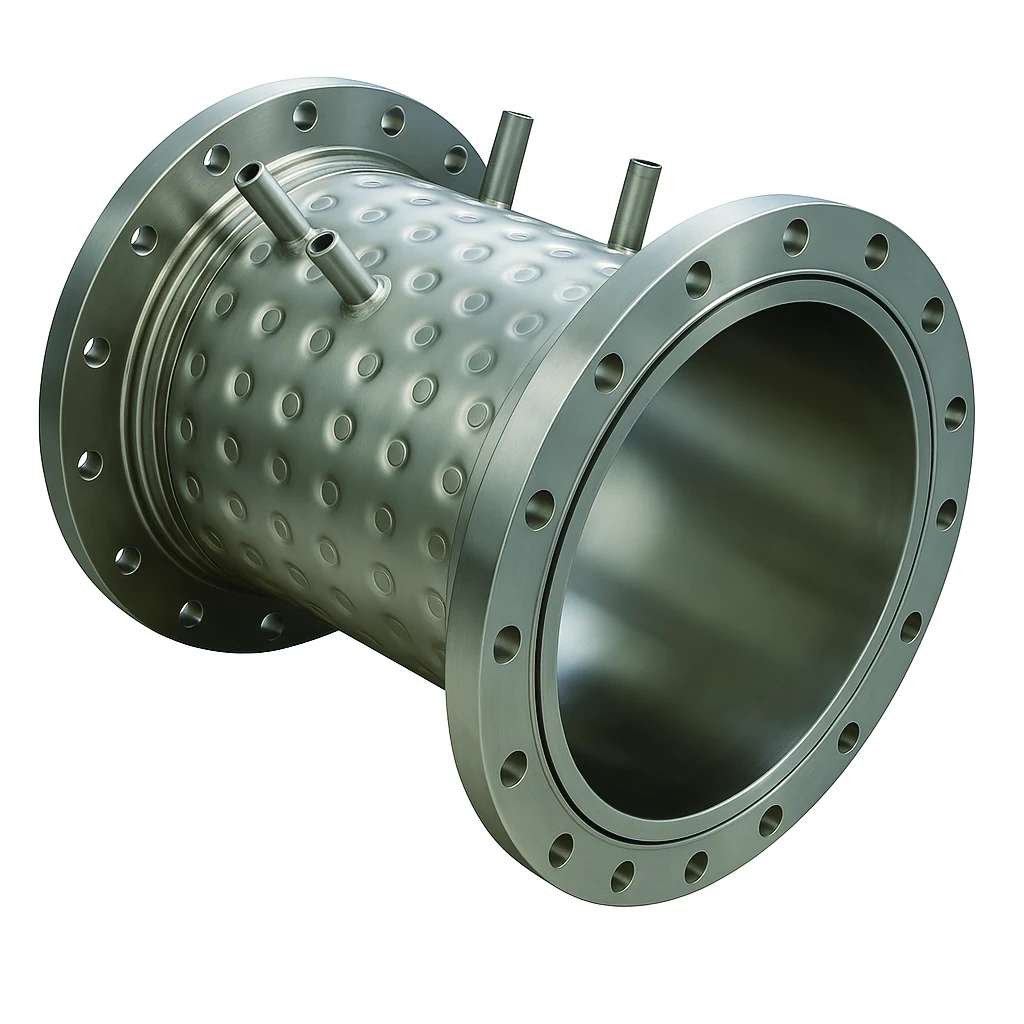
Integrated cylindrical surfaces combine containment geometry with thermal control.
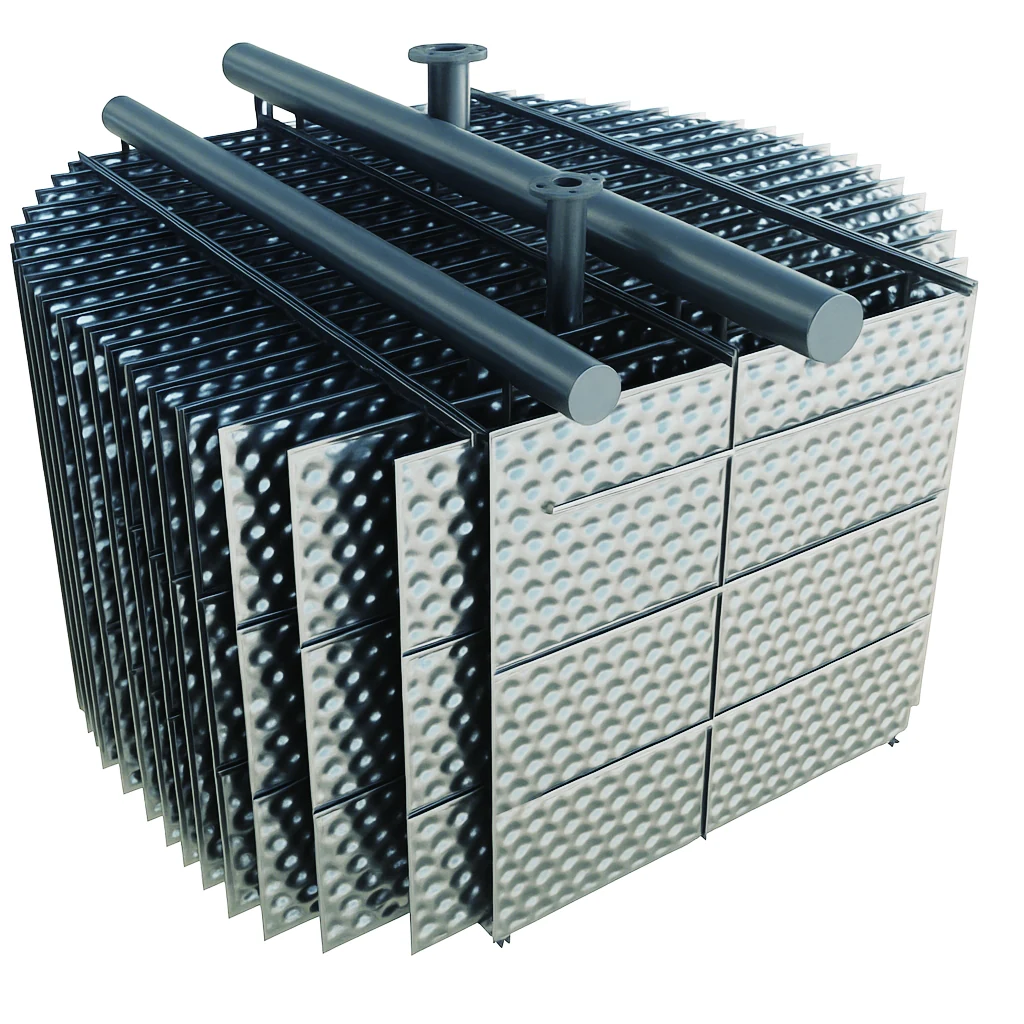
Modular plate banks are arranged around flow, capacity, cleaning and installation space.
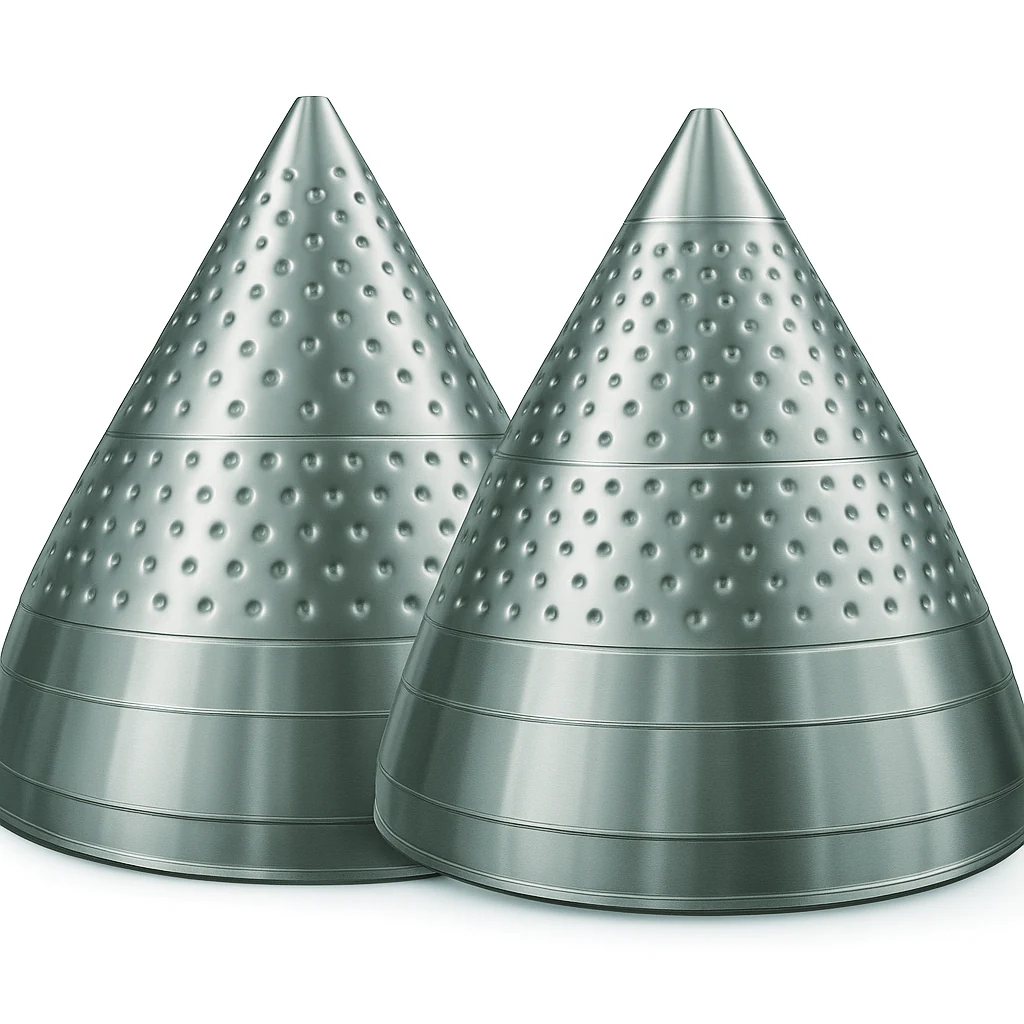
Custom-formed panels extend heat transfer into hoppers and non-cylindrical vessels.
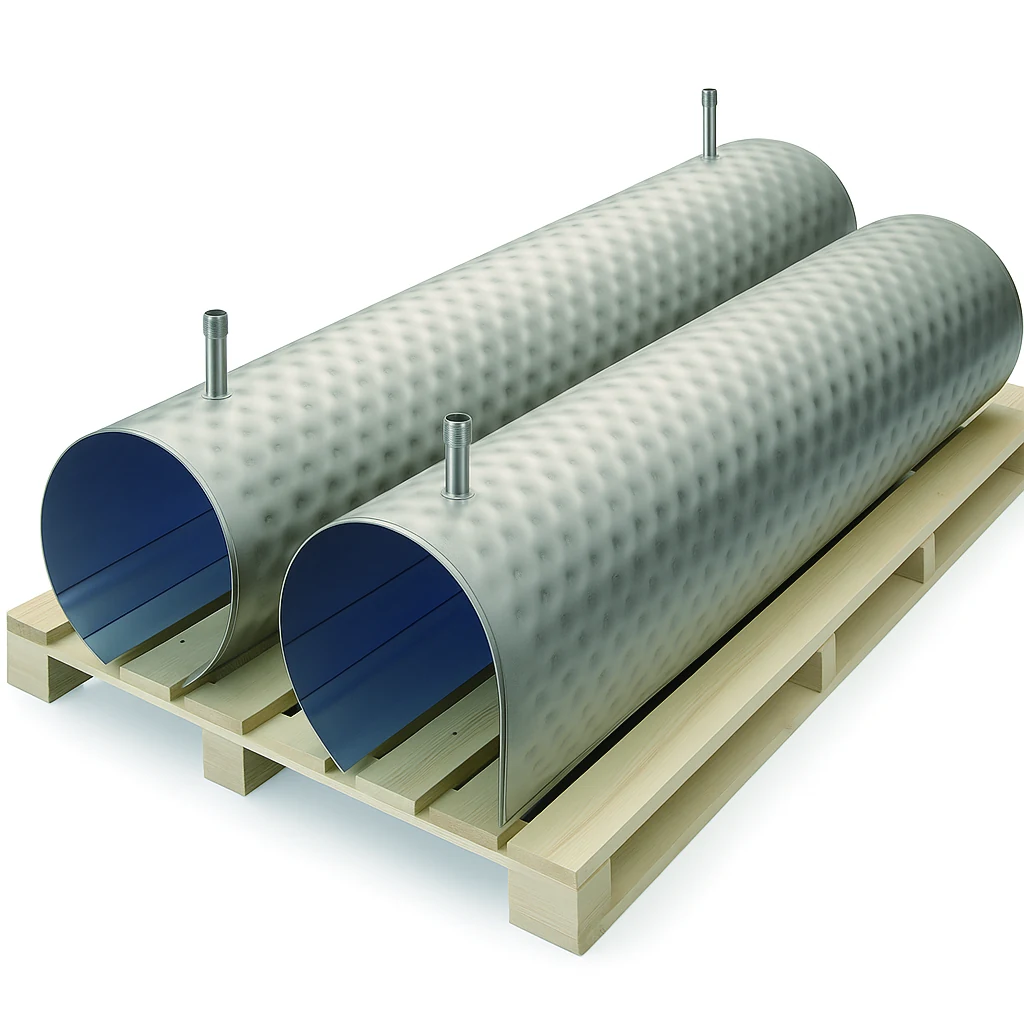
Curved sections support custom thermal surfaces and special fabrication geometries.
Industrial sectors
Pillow plates are especially useful where conventional tubular exchangers are difficult to install, clean or integrate.
Compare single- and double-embossed pillow plates for tank jackets, immersion bundles and falling-film chillers. Provide process and utility media, flow rates, inlet/outlet temperatures, operating and design pressures, allowable pressure drop, material and installation form. Include panel dimensions and available space; for jackets, add tank diameter, heated/cooled height and connection layout. Confirm whether the supply covers panels, a jacket or an assembly.
Selection data
For a tank jacket, include vessel diameter, covered height and the available connection positions. For an immersion bundle, include liquid level, vessel openings, support arrangement and removal space. For a falling-film chiller, identify the liquid distribution arrangement, flow rate, target temperatures and cleaning requirements. Thermal and mechanical design must be checked against the proposed geometry.
Frequently asked questions
Two sheets are laser-welded in a calculated pattern and inflated to form internal flow channels. Heating or cooling media move through those channels while the outer surface transfers heat to a tank, product film or surrounding process.
It is a welded plate pair whose spot and perimeter welds define a pressure-inflated channel. The weld pattern, sheet thickness, inflation depth and connections are engineered for the required flow distribution and mechanical load.
Yes. Single-embossed pillow plates can be formed around cylindrical vessels or integrated into tank walls and bottoms for heating, cooling or temperature control.
Falling-film pillow plate surfaces are used for water, dairy and process cooling duties where liquid forms a thin film over the plate and transfers heat to the cooling medium inside.
Provide panel or vessel geometry, available surface area, process and utility media, flow rates, temperatures, design pressure, material, sheet thickness constraints, installation method and cleaning requirements.
Custom pillow plate engineering